Three years ago, a casthouse owner in North Africa bought the cheapest casting line he could find. It ran, after a fashion — but the billets needed heavy scalping, the customers complained, and the yield never met the brochure numbers. Two years later he was pricing a hot top billet casting machine to replace it, effectively paying for his casthouse twice. This guide is the conversation he wishes he’d had before signing — what actually matters when you buy a hot top billet casting machine, beyond the headline price. Work through the sections below in order, and you’ll have a specification your engineers can defend and your finance team can believe.
Diameter Range and Strand Count
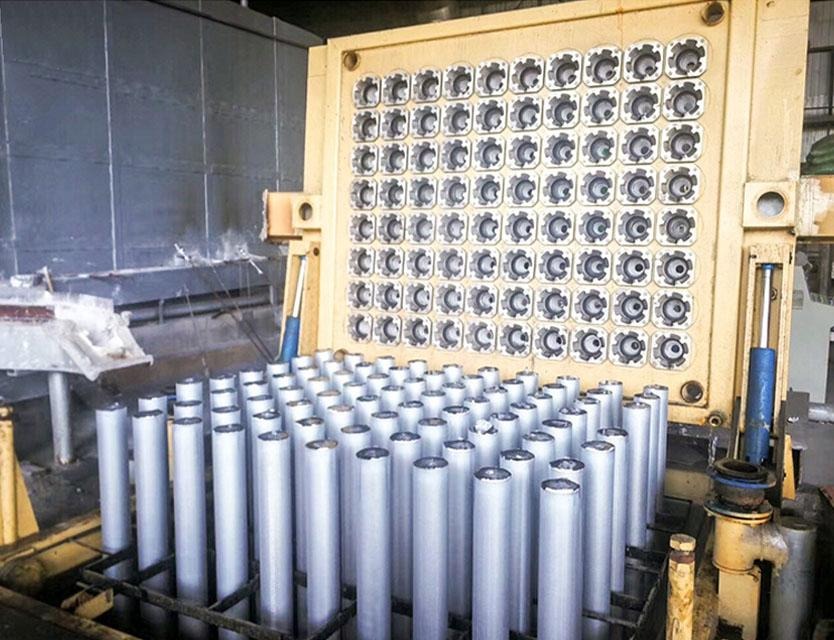
When sizing a hot top billet casting machine, start from your product mix, not the catalog’s maximum. Most suppliers cover billet diameters from around 150 mm up to 500 or 600 mm, with the number of strands (molds casting simultaneously) setting your throughput. A hot top billet casting machine with more strands pours more tonnes per shift, but only if your furnaces can keep up — a twelve-strand machine fed by an undersized furnace is just expensive decoration. Map your top five billet sizes and your annual tonnage first, then buy the configuration that covers them with a little headroom, not the biggest one in the brochure. Also think one alloy generation ahead: if your customers are drifting toward harder 6xxx variants or larger profiles, buy the diameter flexibility now rather than discovering the limit mid-contract.
Automation and Control Systems
Modern versions of the hot top billet casting machine come with PLC-based control: casting recipes stored per alloy and diameter, automatic metal-level control, and data logging of every cast. Ask any plant that upgraded to a hot top billet casting machine with full automation and they will point to the same wins — steadier starts, fewer operator-dependent variations, and a complete traceability record when a customer asks what happened in cast number 4,312. If you run multiple shifts with varying crew experience, automation is not a luxury; it is how you make Monday morning’s billets match Friday night’s. Remote diagnostics are worth asking about too — a supplier who can read your cast data from abroad will usually solve a problem faster than one waiting for a flight.
Cooling System Design
Cooling design separates a good hot top billet casting machine from a troublesome one. Ask how water is distributed — individual flow control per mold beats a single shared header — what inlet temperatures and flow rates the design assumes, and what filtration the supplier recommends. Uniform, controllable cooling is what gives you a consistent shell and a clean surface; an underspecified water circuit gives you breakouts and endless troubleshooting. Get the cooling specification in writing, including the water quality your plant must supply, before the contract does.
Consumables and Wear Parts
Consumables are where a hot top billet casting machine either stays cheap to run or quietly bleeds money. Graphite rings, mold sleeves, gaskets, thermocouples — price a year’s worth before you buy, not after. Ask which parts are proprietary and which are standard: a supplier whose rings only fit their molds owns your maintenance budget for the next two decades. Before buying a hot top billet casting machine, also confirm realistic ring life in casts, not just in the sales presentation, and check that spares ship in weeks rather than months.
Commissioning, Training, and After-Sales
A hot top billet casting machine is a twenty-year asset, and the supplier relationship lasts nearly as long as the steel. Insist on supervised installation and commissioning — the first casts should happen with the supplier’s engineer on the floor, not over a video call. Operator training should cover not just button-pushing but the metallurgy of why each parameter matters; a crew that understands the process runs the machine better than one that only knows the screens. And verify the unglamorous details: spare-parts lead times, service engineer availability in your region, and documentation in a language your maintenance team actually reads.
Total Cost of Ownership
The purchase price of a hot top billet casting machine is only the down payment. The real calculation spans yield gains against the alternative, energy per tonne, labor, consumables, and the cost of unplanned stops. A machine that costs fifteen percent more but lifts recovery by two points and halves your scalping waste pays for the difference within a few years on any serious tonnage — while the cheapest quote in the pile often turns out to be the most expensive machine you ever buy. Run the ten-year numbers honestly, and buy the hot top billet casting machine that fits your metal, your people, and your customers. That is the one that will still be earning its keep when the cheap line is already being replaced.